What Is Steam Trap Testing?
Steam trap testing methods include visual inspection, surface temperature checks, contact ultrasound or acoustic testing, and observation through a purpose-designed sight glass or monitoring device. The most useful approach combines the readings with three facts: the trap type, whether steam is available at the inlet, and whether the equipment is producing condensate. A single hot reading or a short burst of noise is not enough to diagnose a failure.
Steam traps discharge condensate and help limit the escape of live steam. When a trap leaks, the plant can lose energy without seeing an external plume. When condensate cannot drain, the equipment may heat slowly or unevenly. Finding the difference helps a maintenance team decide whether to investigate the trap, the steam supply or the condensate return system.
Why Test Steam Traps Under a Known Load?
Sound and temperature change as a process starts, reaches temperature, idles or stops. A cold trap on an isolated branch does not tell you how it would behave in service. Similarly, a quiet trap at low load may be between discharge cycles. If you cannot establish the operating state, mark the result as inconclusive and return when the equipment is running.
Different designs also produce different patterns. An inverted bucket steam trap can discharge intermittently. A float and thermostatic trap may discharge more continuously under a steady load. Continuous flow on its own is not proof that a float trap is passing live steam, just as cycling alone does not prove an inverted bucket trap is sealing correctly.
What Can a Steam Trap Test Reveal?
A routine survey can flag a trap that appears to operate normally, one that may be leaking or blowing through, and one that is cold or not draining as expected. Treat these as findings to interpret. For example, a cold trap could reflect a closed isolation valve, a restriction, or a genuine failure. High back pressure can also prevent drainage even when the trap mechanism works.
Keep live steam and flash steam separate in your diagnosis. Hot condensate can form flash steam when its pressure drops. Vapour in an approved observation point may therefore occur during normal discharge. Compare the pattern with the trap design and the process load before deciding that a plume, a hot return line or a noisy outlet indicates live steam leakage.
When Should Maintenance Teams Test Steam Traps?
Use consistent steam trap testing methods to compare readings over time, but set the survey interval according to plant risk. Give greater priority to units serving critical heat exchangers, continuously operating steam mains and processes where poor drainage affects product quality or production. Also schedule a check after an unexpected heating problem, recurring condensate backup or repair.
A practical survey route groups equipment by area and expected operating window. A batch reactor may need to be checked during a representative heating stage, while a main drip trap can be assessed when the distribution line is in service. Coordinate with operations so an idle branch is not mistaken for a failed trap and important test opportunities are not missed.
How to Test Steam Traps and Act on the Findings
Method 1 – Visual Inspection and Operating Checks
Confirm the tag, trap type, equipment duty and reported operating state. Look from an approved position for obvious external leakage, damaged supports, unusual vibration or signs of poor drainage. Review accessible pressure readings and the status of the steam supply and return system. Visual checks help decide where to investigate, but they do not establish whether a closed-return trap is leaking internally.
Follow plant safety procedures and use approved access and test points. Never loosen a fitting or open a pressurised trap to look for discharge. Any inspection requiring disassembly must follow the site’s isolation, depressurisation and cooling procedures.
Method 2 – Contact or Infrared Temperature Checks
Measure the surface temperature at consistent, accessible points specified in the testing procedure. Compare the inlet and outlet readings with the steam pressure and the operating state. An unexpectedly cool inlet during a confirmed heating duty calls for a supply or flow check. A hot outlet can occur with normal hot condensate or flash steam, so temperature alone does not reliably confirm leakage.
For non-contact infrared measurements, use a suitable target surface and follow instrument guidance on emissivity and distance. Shiny metal and inconsistent target locations can produce misleading comparisons. Record the measurements as surface temperatures, not direct measurements of the steam or condensate inside the pipe.
Method 3 – Contact Ultrasound or Acoustic Testing
A contact ultrasonic or acoustic instrument picks up sound transmitted through the metal as steam or condensate moves. Use the manufacturer’s recommended measurement point and listen long enough to catch the expected discharge pattern. For an intermittent trap, listen between cycles as well as during discharge. An unusually persistent signal can justify further investigation, especially when the trap would normally close between cycles.
Compare the reading with adjacent pipework if a nearby control valve, pump or trap may be contributing noise. There is no universal sound level that identifies a failed trap across all types and pressures. Use the test instrument correctly and judge the signal alongside temperature, load and the normal behaviour of that model.
Method 4 – Sight Glass or Installed Monitoring
A pressure-rated sight glass installed for the purpose can help an operator observe discharge without opening the circuit. It provides visual context, but flash steam and changing condensate loads still make interpretation important. Where repeated manual access is difficult or the service is critical, a suitable monitoring system can help flag changes between surveys. Select the device and its location for the installation rather than assuming one method fits every duty.
Bring the Readings Together in a Steam Trap Survey
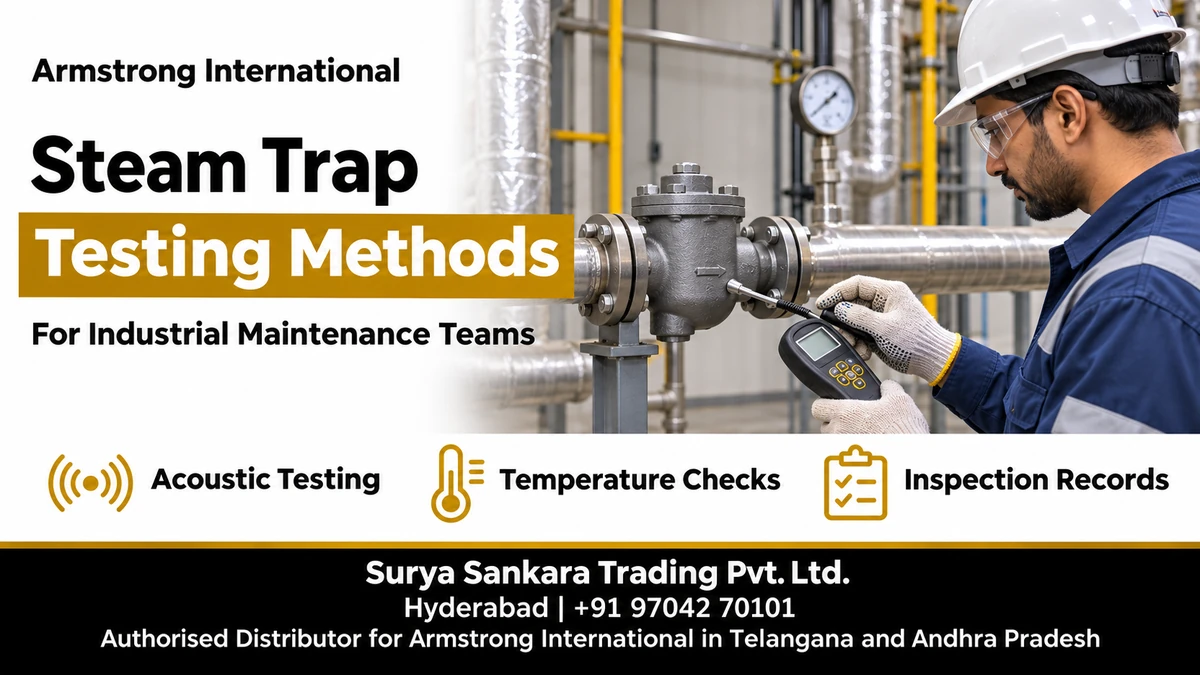
For most portable surveys, combine steam trap testing methods rather than relying on one reading. Start with an operating check, then compare temperature and acoustic results. The Armstrong International SAGE UMT® steam trap tester combines a contact acoustic sensor with non-contact infrared temperature measurement. It can transfer results to SAGE® for recording and review. See Armstrong International’s official steam trap testing guidance for the manufacturer’s description of the instrument and its survey workflow.
Record What the Next Technician Needs to Know
- Trap ID, location, model or type, and the equipment it serves.
- Date, load condition and available inlet or return pressure readings.
- Test method, measurement locations, temperatures and observed acoustic pattern.
- Assessment, confidence level, suggested follow-up and the responsible team.
If the readings disagree, note the uncertainty rather than forcing a pass or fail result. For example, a hot outlet and a brief acoustic burst on a cycling trap may be normal discharge. A hot outlet paired with sustained flow noise warrants a closer check if the trap should be closed under those conditions. Compare with a known-good unit of the same type operating under similar conditions where practical.
Retest After Corrective Work
Prioritise confirmed faults by their impact on production, energy use and maintenance risk. After repair, replacement or correction of a supply or return problem, retest under a comparable operating load. Log the outcome against the same tag. That closes the work order with evidence and makes repeat problems easier to spot.
Frequently Asked Questions
Which steam trap testing methods work best in a running plant?
Contact ultrasound or acoustic testing combined with a temperature check and a known operating load is a practical survey approach. Choose test points and interpretation criteria for the trap design and site conditions.
Does a hot steam trap outlet mean the trap has failed?
No. Hot condensate and flash steam can keep the outlet warm during normal operation. Check the discharge pattern, load and acoustic readings before diagnosing a live steam leak.
What should I do if a steam trap is cold while the process is running?
Confirm the equipment is calling for heat, steam is available at the inlet and the trap is in service. Investigate supply restrictions, drainage conditions and return back pressure before concluding the trap itself has failed.
Can healthy steam traps sound different from each other?
Yes. The trap design, steam pressure and condensate load all influence the sound. Compare similar trap types under similar conditions and observe the complete discharge pattern.
Where can I enquire about Armstrong International steam trap testers?
Contact Surya Sankara Trading Pvt. Ltd. in Hyderabad for Armstrong International steam trap testing equipment enquiries in Telangana and Andhra Pradesh. Share the types and approximate number of traps, your application and the problem you want to investigate.
Steam Trap Testing Equipment Enquiries in Telangana and Andhra Pradesh
Surya Sankara Trading Pvt. Ltd. is an Authorised Distributor, Business Associate and Channel Partner for Armstrong International in Telangana and Andhra Pradesh. To discuss a steam trap tester for your plant, call +91 97042 70101 or send your requirements on WhatsApp.